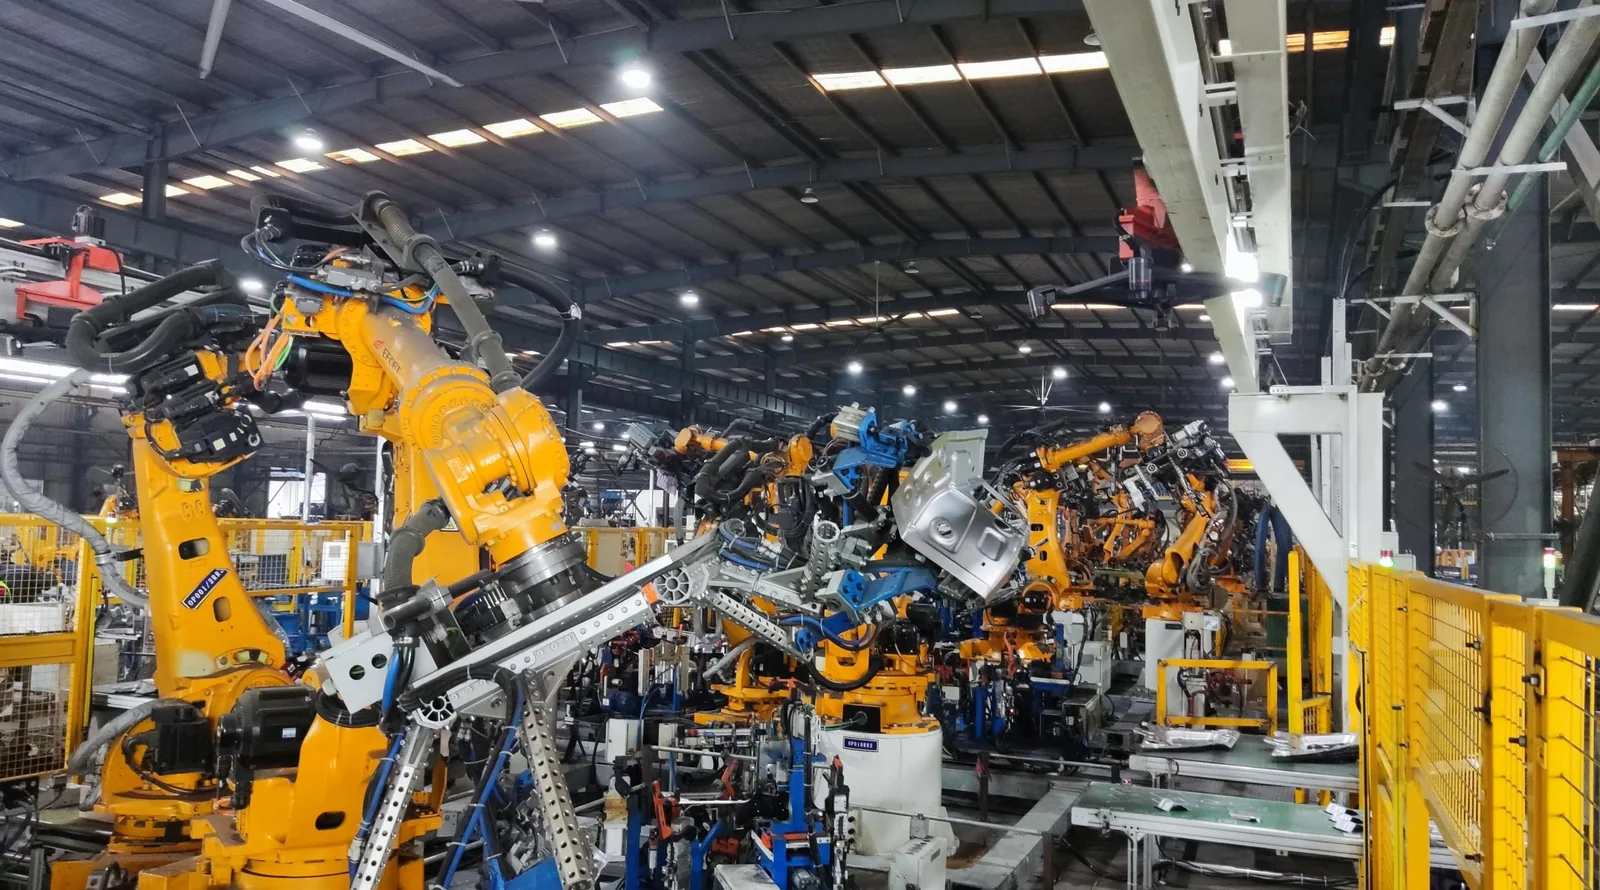
Body-shop retooling for a model change — about 180 welding stands, priced and commissioned stand by stand
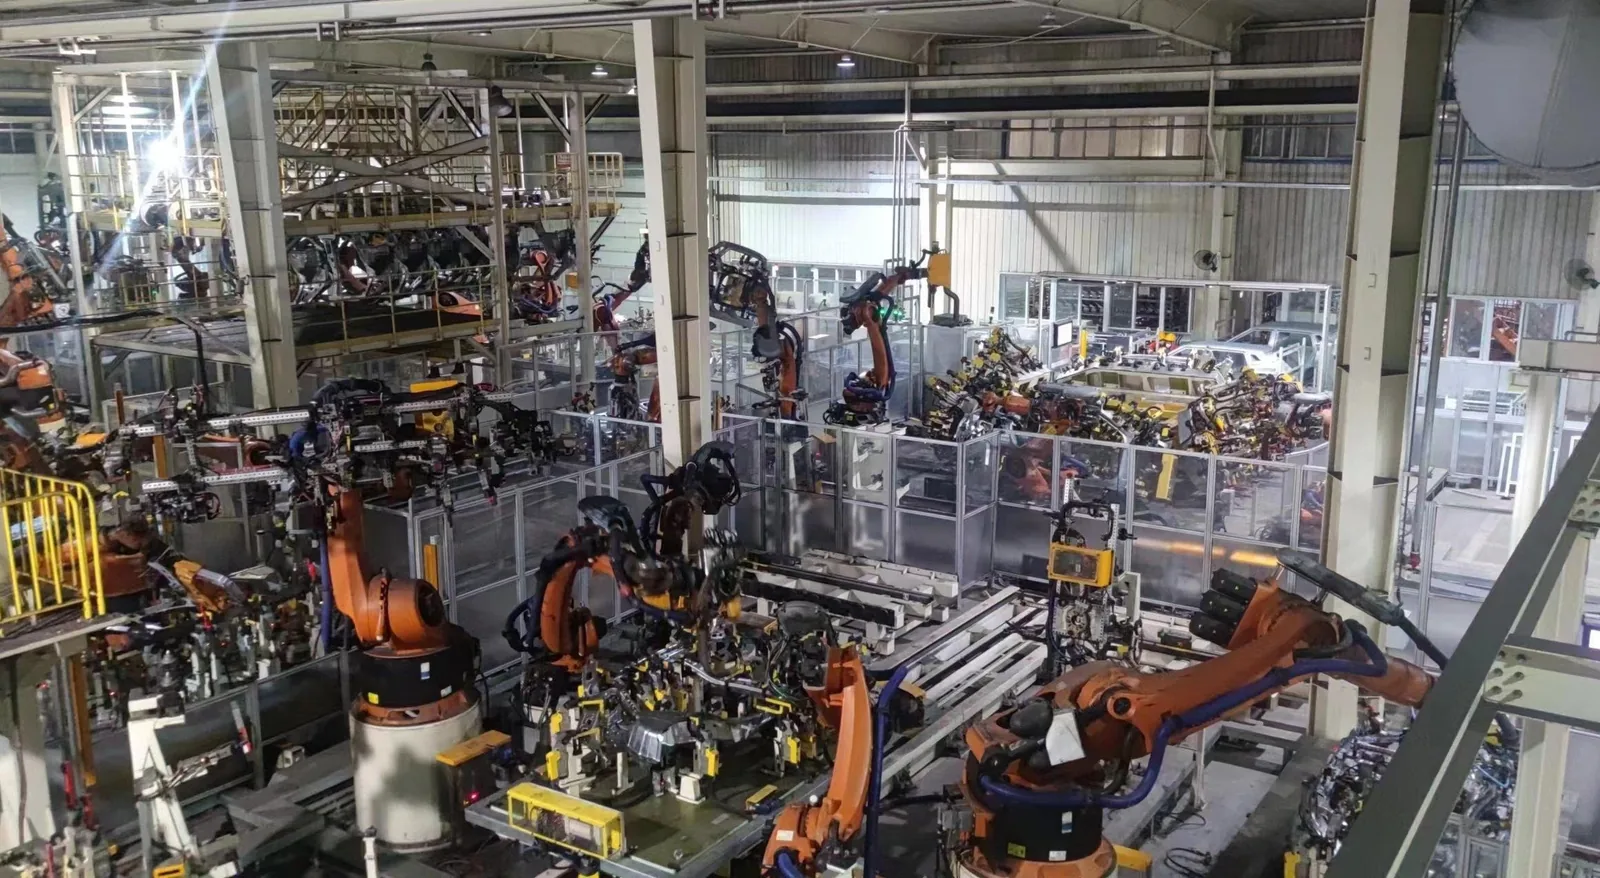
A model change at a passenger-car plant in north-west Russia: about 180 welding stands, hanging jigs and special stations — wheel-arch hemming, door inner-panel welding, boot-lid mastic application — newly built or renovated, with pneumatic and electrical control converted to a jig-box scheme. Every item was matched to the plant's own asset codes and priced with its own installation and commissioning line, so the changeover could be staged shop by shop instead of stopping the line as one.
The problem the customer brought
A whole shop had to change model while continuing to produce, and the plant's finance and maintenance departments needed the package in the form of their own asset register, not as a supplier's lump sum.
Workpiece
Passenger car body in white — sub-assembly and main-line welding stands across the shop, plus wheel-arch hemming, rear and front door inner-panel welding and boot-lid mastic stations.
Robots
None supplied. Existing shop equipment retained; the work was tooling, control conversion, installation and commissioning.
Process and equipment
About 180 welding stands, hanging jigs and special stations newly built or renovated; manual clamping converted to pneumatic and electrical control on a jig-box scheme with clamp sequencing, two-hand start, safety circuit and station HMI. Mechanical and electrical spare-parts lists delivered with the project.
Pre-integration and factory acceptance test
Each stand accepted on its own: installation and commissioning were separate priced items per asset code, so acceptance followed the shutdown sequence rather than a single line acceptance.
Delivery and site work
Delivered in batches to suit the plant's shutdown windows. Design changes during execution were quoted item by item against the same asset codes. An in-plant relocation of the line followed after hand-over.
Commercial terms
Contract appendix listing equipment and works line by line against the customer's asset codes, each with its own installation and commissioning item. Prices are not published.
Shipping terms on current projects: EXW, FOB, CIF or DAP. Customer names, plant locations and prices are not published.
Result
Delivered, with the design-change packages and the later relocation handled under the same documentation. Built by our body-shop partner; the customer interface, commercial documents and export chain were ours.
What we do differently because of this project
Retooling is now always quoted against the customer's own asset register, with installation and commissioning priced per item. It is the only format that lets four departments in a car plant use the same document.
Photographs from this project
Customer names, plant identification and location watermarks are removed. Captions state where an image is a general illustration rather than this customer's plant.