
Welding fixtures and tooling packages
You keep your robots and your welding equipment; we supply the tooling that makes the new model — every station fixture, the shared base plates, hangers, rotary and hemming tooling, and the station control that sequences the clamps and talks to your robot. Designed from your 3D data, built and pre-assembled in China, key fixtures inspected on a coordinate measuring machine, priced station by station so you can see and phase what you are buying. This is how all three of our body-shop projects were bought, two of them by the same plant.
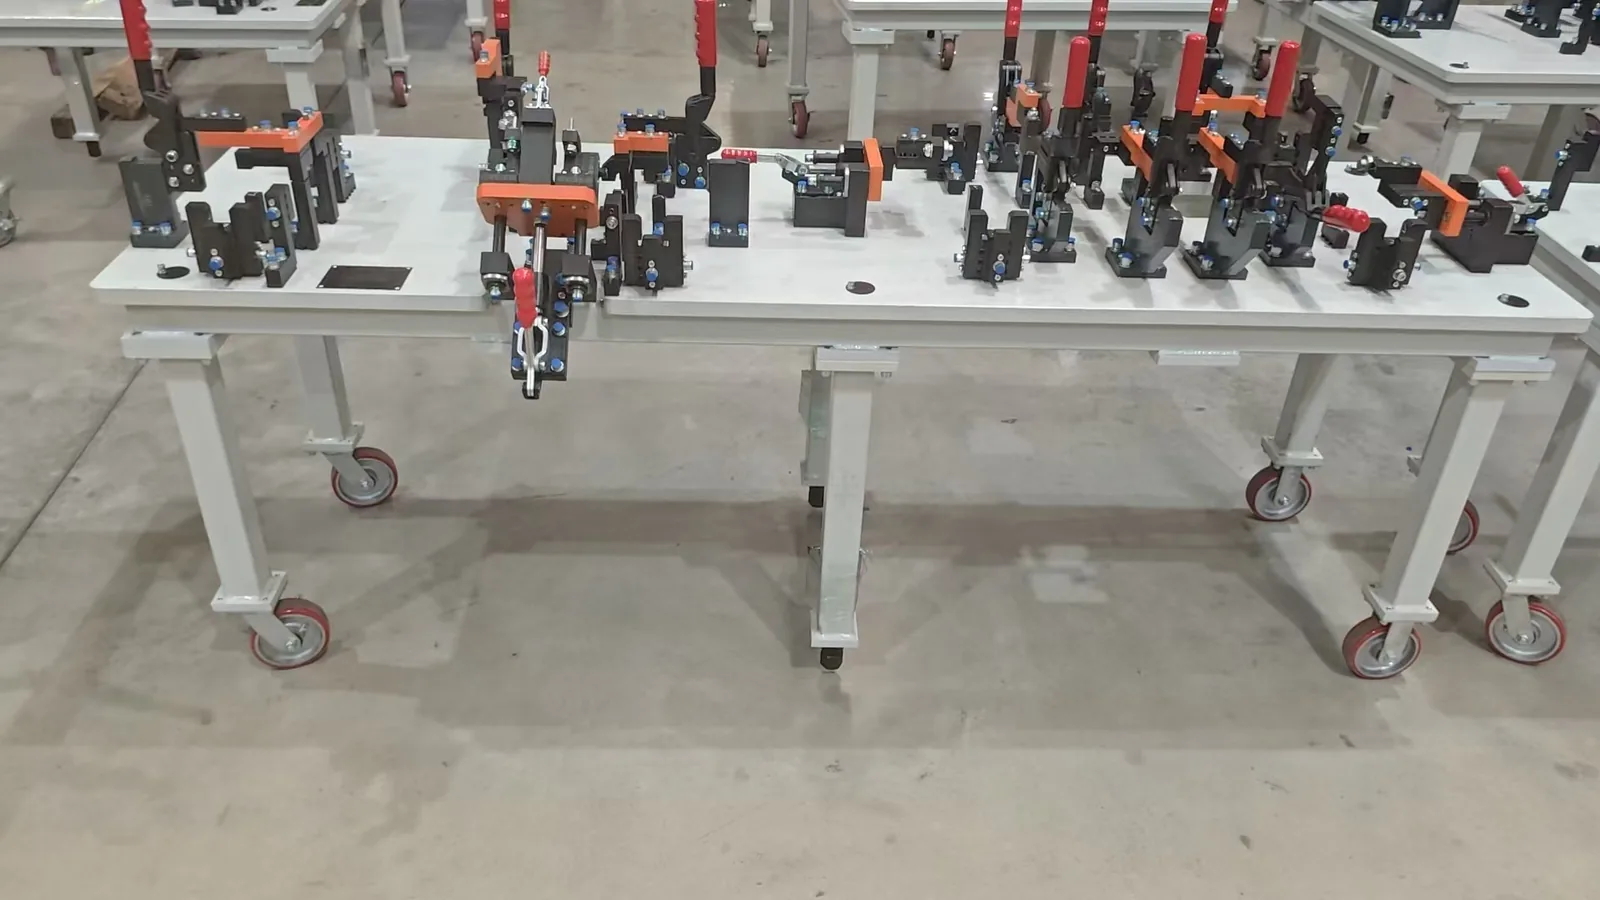
What is in a tooling package
| Item | What it does |
|---|---|
| Assembly and welding stand | The workhorse: a welded and machined frame carrying NC blocks, clamps and pins that hold the panels in position while they are joined. |
| Robot welding fixture | The same, arranged so a robot can reach every joint — clamp positions, cable routing and the safety interface are part of the design. |
| Shared base plate | A machined base carrying two or more fixtures, so small sub-assemblies share one floor position and one set of datums. |
| Hanging jig and hanger | Carries a sub-assembly between stations on a hoist or monorail; the plant normally supplies the hoist, track and steel structure. |
| Rotary and turnover fixture | Manual or powered, so one operator can weld both sides without re-fixturing. |
| Hemming tooling | Roller or table hemming for doors, hood, tailgate and wheel arches. |
| Sealing and mastic station | Heated pump, applicator and the fixture that presents the part to it. |
| Checking fixture | Where the plant wants a dedicated gauge rather than a measuring machine. |
| Station control | Pneumatic valve island, clamp sequencing, two-hand start, safety circuit and the HMI for the station. |
Not in the package, unless you ask for them: robots, spot guns and transformers, arc sets, stud units, positioners, fume extraction, safety fencing and the hoists themselves. We can supply any of them — they are simply quoted as separate lines so the tooling price stays readable. The full scope split →
What we need to design it
| Input | What it is | Status |
|---|---|---|
| Body 3D data | STEP, CATIA or JT of the panels and the sub-assemblies, in the vehicle coordinate system. | Required |
| Joining information | Weld-spot and weld-seam layout, adhesive and sealer paths, stud positions. | Required |
| Station split | Which sub-assembly is welded where — or ask us to propose it from the part list. | Required or proposed |
| Existing equipment | Robot brand, model and controller; welding sets; positioners; hoists; the fencing you already own. | Required |
| Layout | Shop drawing with the floor positions, hoist tracks, column pitch and clear height. | Required |
| Datum and tolerance | The RPS or datum scheme and the tolerances the sub-assembly has to hold. | Required |
| Standards | Plant standards for pneumatics, electrics, safety and labelling, if you have them. | If they exist |
| Rate and shift | Parts per hour at the station, shift pattern, and whether a second model shares the fixture. | Required |
With those in hand a concept and a quotation come back within one week. Without the 3D data nothing honest can be quoted, and a supplier who quotes anyway is guessing with your money.
How a tooling package is executed
- Station split and concept — which sub-assembly is welded where, how many fixtures each station needs, what is shared on a common base plate.
- Design and review — 3D design of every fixture against your datum scheme, released to you for review before anything is cut.
- Manufacture — frames welded and stress-relieved, machined on gantry centres, locators and clamps fitted.
- Inspection — key fixtures measured on a coordinate measuring machine against the drawing; the report ships with the fixture.
- Pre-assembly and inspection round — the stations are assembled in the workshop and presented for your inspection before packing.
- Packing and export — packing list, container loading plan, export documents and freight on the term you choose.
- Installation — our engineers set the fixtures to the datums with a laser tracker, connect the station control and tune the clamping sequence.
Delivered tooling packages
- BIW tooling package for an electric model — 65 fixture sets, 29 stations — Russia, 2024.
- A second model at the same plant — 54 fixture sets, 20 stations — Russia, 2026.
- Body-shop retooling for a model change — about 180 welding stands — Russia, 2025.
Quantities counted from the quotations and contract appendices. Customer names, contract values and locations below country level are not published. All three, in full →
Best price on enquiry. We do not publish prices. A body-shop package is priced against your body data, the line rate, the number of models sharing the line and the scope split — those move the figure far more than any list price could. Send the requirement and you get an itemised offer, on EXW, FOB, CIF or DAP terms.
Frequently asked questions
What is a tooling package, exactly?
Everything that holds and positions the part, and nothing that joins it. Fixtures, shared base plates, hangers, rotary and hemming tooling, the station control that sequences the clamps, and the interface to your robots and welding sets. You keep the robots, the guns and the welding equipment you already own.
Why would we buy tooling without robots?
Because for a model change it is the cheapest way to production. Your robots are not the thing that stops you building a new body — your fixtures are. All three body-shop projects we have delivered were bought this way, including two by the same plant.
How is it priced?
Per station, itemised. Every fixture is a line with its own price, so you can see what each station costs, move a station out of scope, or phase the order. That is how our quotations to Russian plants have been written and it is how yours will be.
Do you design the fixtures or do we?
We do, from your 3D data and datum scheme, and you review the design before it is cut. If your engineering department prefers to design and have us build, that works too — say so with the enquiry.
How accurate are they?
Key fixtures are inspected on a coordinate measuring machine against the drawing and the report ships with them; installation datums are set on site with a laser tracker. The tolerance the sub-assembly has to hold is agreed before design starts, not argued about at acceptance.
Can we see them before they ship?
Yes. The fixtures are assembled and, where robots are in scope, taught and cycle-verified in the builder’s workshop. On our second project for the same plant a payment milestone was tied to that inspection round in China.
What about installation?
Our engineers come and set the fixtures to the datums, connect the station control, tune the clamping sequence and hand over. Your plant supplies the cranes, riggers and electricians.
Which robot brands can the station control talk to?
Whatever is in your plant. The station control, safety circuit and the robot interface are designed around the controller you already run.
Send a body-shop enquiry If the whole shop has to change over